
Fluidline
NPT, BSPT or BSPP ‘G’? Why the thread you choose decides whether your connection seals
Three pipe threads. Near-identical sizes. Completely different ways of sealing. Getting them mixed up is one of the most common causes of leaks we see on instrumentation installs across Africa, and it usually shows up at pressure test.
A 1/2″ NPT male and a 1/2″ BSPT male both have 14 threads per inch. Hold them side by side and most people can’t tell them apart. Screw one into the other’s port and it will often go two or three turns, then feel tight, which looks a lot like a good connection. It isn’t. The thread forms don’t match, and the connection can weep, or fail outright, once the system is pressurised.
Quality tube fitting and pipe fitting manufacturers, including Uni-Lok, which Fluidline distributes, all offer these end connections side by side, and they all publish thread identification guides for the same reason: the thread is where the tube fitting meets the rest of the plant, and a perfect compression connection doesn’t help if the pipe-thread end leaks.
The three threads at a glance
What each thread looks like
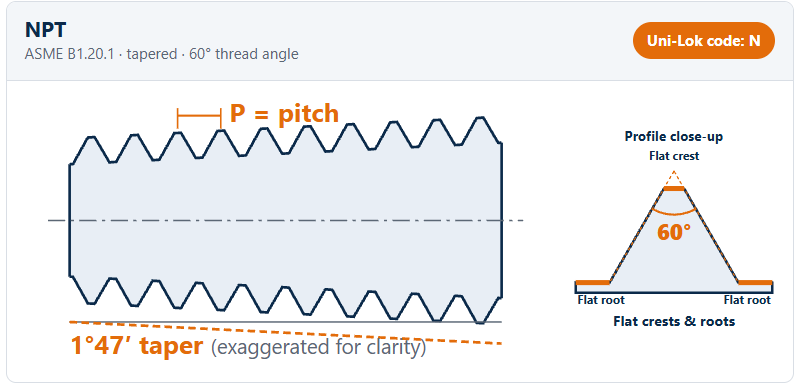
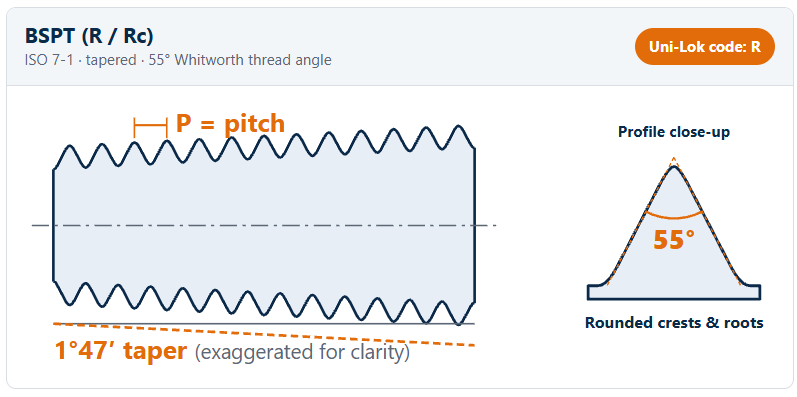
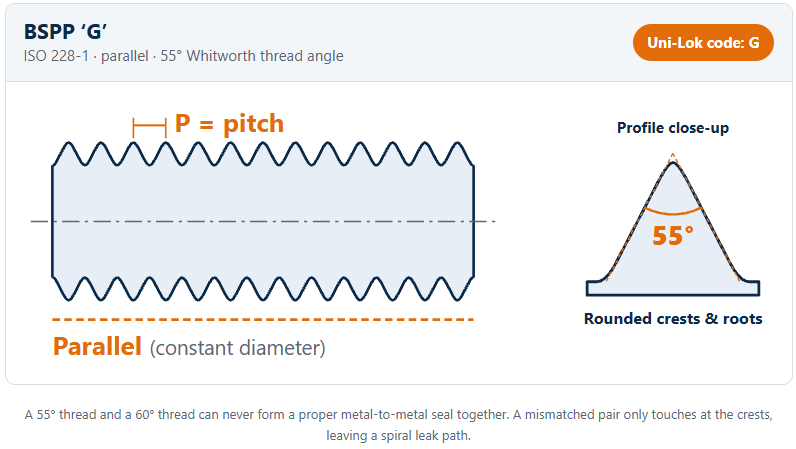
The differences are small to the eye but decisive in service. The drawings below are redrawn from Uni-Lok’s pipe thread data.
Tapered threads: NPT and BSPT
Both NPT and BSPT taper at 1:16 on diameter. As the male is tightened into the female, the flanks wedge together, and it’s this metal-to-metal interference that makes the seal. The tighter the fit, the harder the flanks bear on each other.
PTFE tape or a thread paste is used on every tapered connection, but in my experience its main job isn’t to “make” the seal. It lubricates and protects the threads, stopping stainless-on-stainless threads from galling as they’re tightened. It also fills the tiny clearances at the crests and roots, and it makes the connection much easier to make up and to remake later without damaging the thread form. Tape is not a guarantee of a seal. It won’t rescue a mismatched thread or a badly made-up connection.
“Tape is there to protect the threads and make the connection easy to make up and remake. The seal comes from the right thread, correctly engaged.”
NPT (60°)
The American standard. Flat crests and roots, 60° flank angle. Pitch differs from BSP at most small sizes (18 TPI at 1/4″ and 3/8″, versus 19 for BSP), so there the mismatch is obvious. At 1/2″ and 3/4″ both standards use 14 TPI, and that’s where most mix-ups happen. (Don’t confuse NPT with NPTF “Dryseal” threads, which are made to seal through crest-to-root interference without sealant.)
BSPT (55°): R, Rc and Rp
The British/ISO taper thread uses the Whitworth 55° form with rounded crests and roots. ISO 7-1 uses three symbols that are worth knowing:
- R: taper male thread (what’s on a BSPT male connector)
- Rc: taper female thread (taper-into-taper, the strongest seal)
- Rp: parallel female thread made to ISO 7-1 tolerances, designed to accept an R taper male and seal on the threads
Rp is a common source of confusion because it looks like a ‘G’ thread. It isn’t: Rp is part of the pressure-tight-on-the-threads system, while G is not.
Parallel threads: BSPP ‘G’ (ISO 228-1)
A G thread is a straight 55° thread with the same pitch as BSPT. The key difference is that ISO 228-1 threads are not designed to seal on the thread. The thread only holds the parts together. The seal is made by something else, usually:
- a bonded seal (metal washer with vulcanised elastomer lip, often called a Dowty washer)
- a captive elastomeric (ED) seal on the fitting, as used in ISO 1179 / DIN 3852 Form E ports
- an O-ring, or a flat metal or PTFE gasket (copper, stainless or PTFE) compressed against the port face
- Because the seal sits on a face, you don’t need thread tape. In fact, tape or paste on a G thread can stop the face seal from seating and cause a leak. Check the elastomer against your temperature and media. As a guide, NBR is typically suited to about −40 to 110 °C and FKM to about −28 to 204 °C.
Parallel ports have a practical advantage: the fitting can be tightened in any orientation without the “one more turn” problem of taper threads, and they give excellent seal and reseal capability, so they can be remade many times without wearing the port.
Pressure: the thread end often sets the limit
For a fitting with a tube end on one side and a pipe thread on the other, the maximum allowable working pressure is set by whichever end connection has the lower rating. On many fittings that’s the pipe thread, not the tube end. Uni-Lok publishes these reference ratings at ambient temperature, with tapered-thread ratings based on ASME B31.3:
NPT OD shown is the pipe OD. On a tapered male, measure at the 4th–5th full thread from the end, which will read slightly smaller. Bold rows share a pitch, so check the thread angle there.
Identify any thread in 60 seconds
You need a vernier caliper, a pitch gauge (with both 55° and 60° leaves) and a thread ID chart.
- Taper or parallel? Measure the OD at the first full thread and at the last. If the diameters differ, it’s tapered (NPT or BSPT). If they’re the same, it’s parallel (G, or an Rp female). A parallel male usually also has a flat seal face or undercut for a washer.
- Measure the OD (male) or ID (female) and match it to the nearest nominal size in the table above.
- Check the pitch. 18 vs 19, or 27 vs 28 TPI, tells NPT from BSP at most small sizes straight away.
- At 1/2″ and 3/4″, check the angle. Seat the 55° and the 60° gauge leaf in turn. Only the right one sits without light showing through. Flat crests mean NPT, rounded crests mean BSP.
- Confirm with the part number. The end-connection code in the fitting’s catalogue number should match what you measured (see below).